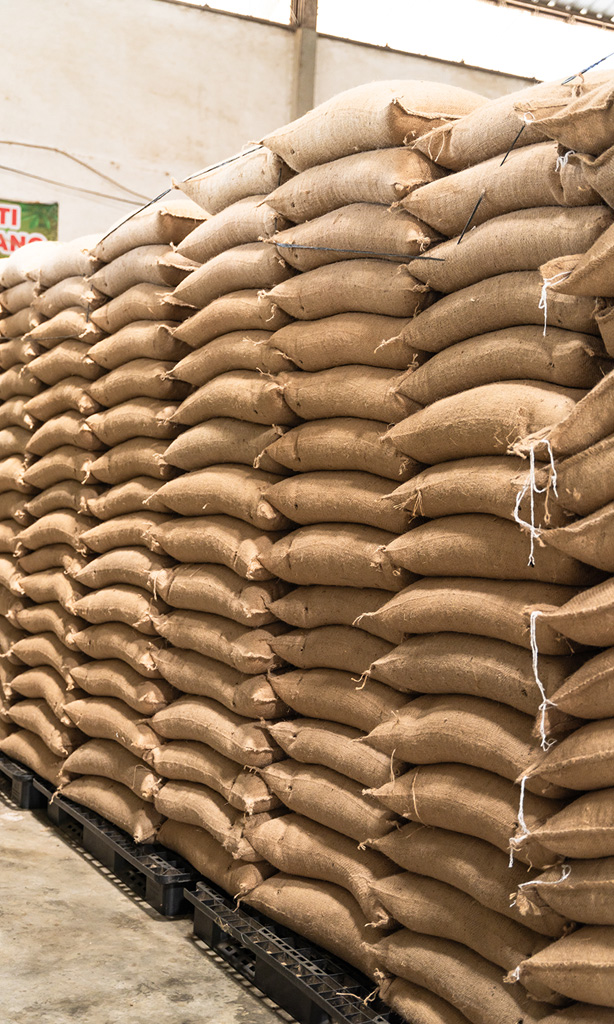
At Mal Agri Coffee, we believe that quality green coffee begins with the right people, efficient operations, and a strong quality control system. From receiving coffee at our warehouse to preparing shipments for customers, every process is managed carefully to ensure consistency and reliability.
Warehouse Operations Team
Our warehouse team is responsible for handling and preparing coffee through:
Quality Control Team
Quality is monitored throughout every stage of the process through:
Administration & Shipping Team
Our administration team supports daily operations through:
By combining experienced personnel with strict quality control procedures, Mal Agri Coffee ensures that every lot of green coffee beans meets consistent standards for both domestic and international markets.
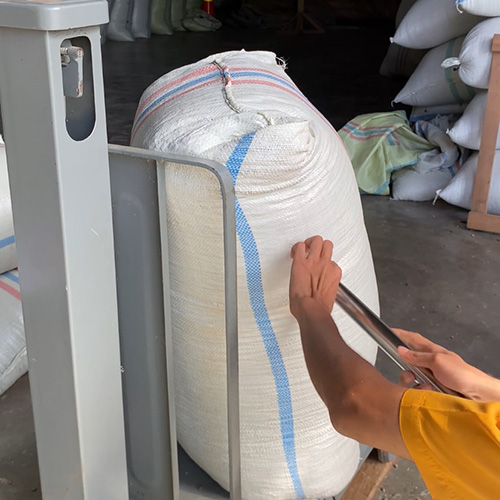
We carefully source green coffee from selected producing regions in Sumatra. Each coffee is evaluated based on its origin, physical quality, and consistency to ensure a reliable supply and maintain the distinctive characteristics of every origin.
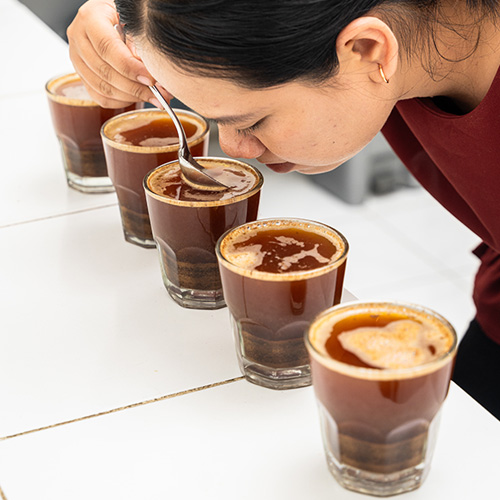
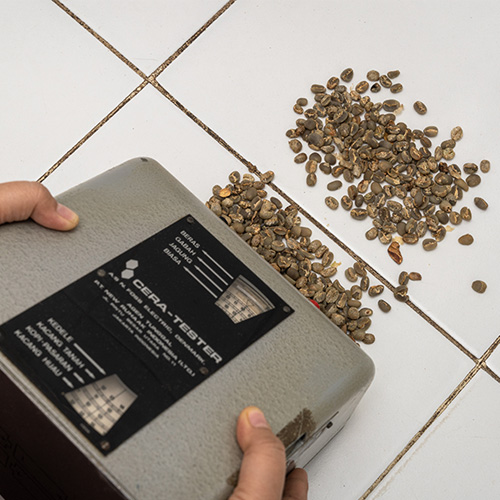
Every lot of green coffee is inspected upon arrival at our facility. We check key factors such as moisture content, physical condition, and overall quality to ensure the coffee meets our standards before entering the next processing stage.
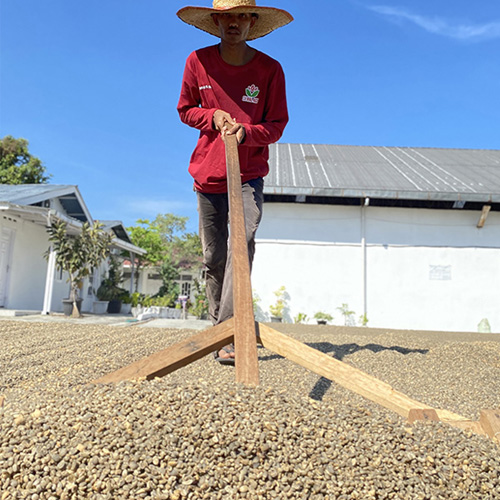
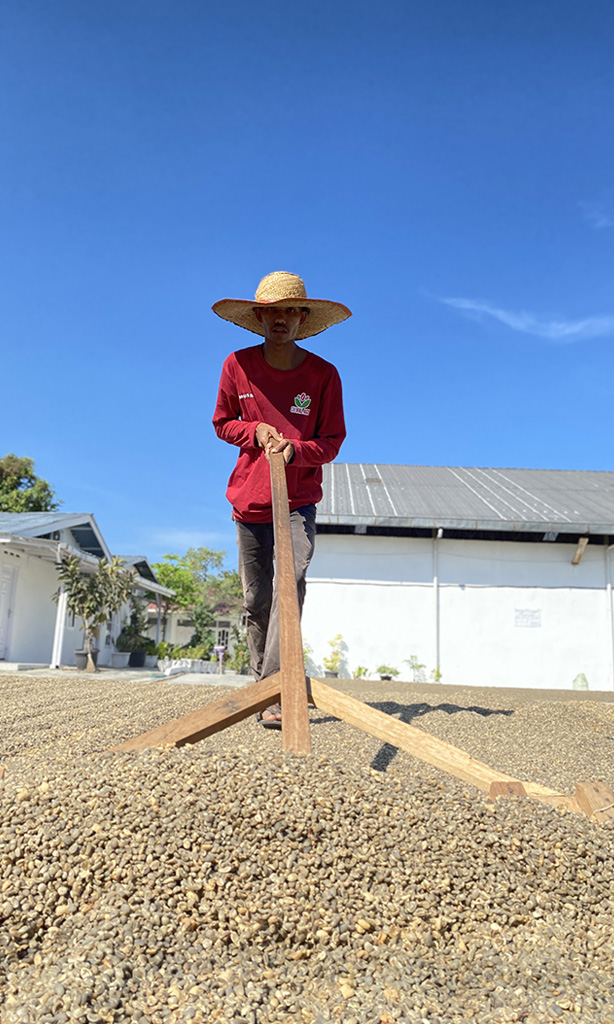
Drying is a crucial step in maintaining green coffee quality. Our coffee is dried under controlled conditions to achieve optimal moisture content and meet international export standards. With a drying capacity of up to 10–12 tons per day, each lot is regularly monitored to ensure stability, optimal shelf life, and the preservation of each origin's distinctive flavor characteristics.
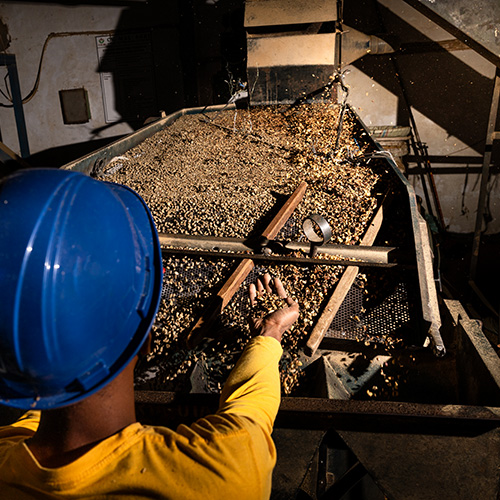
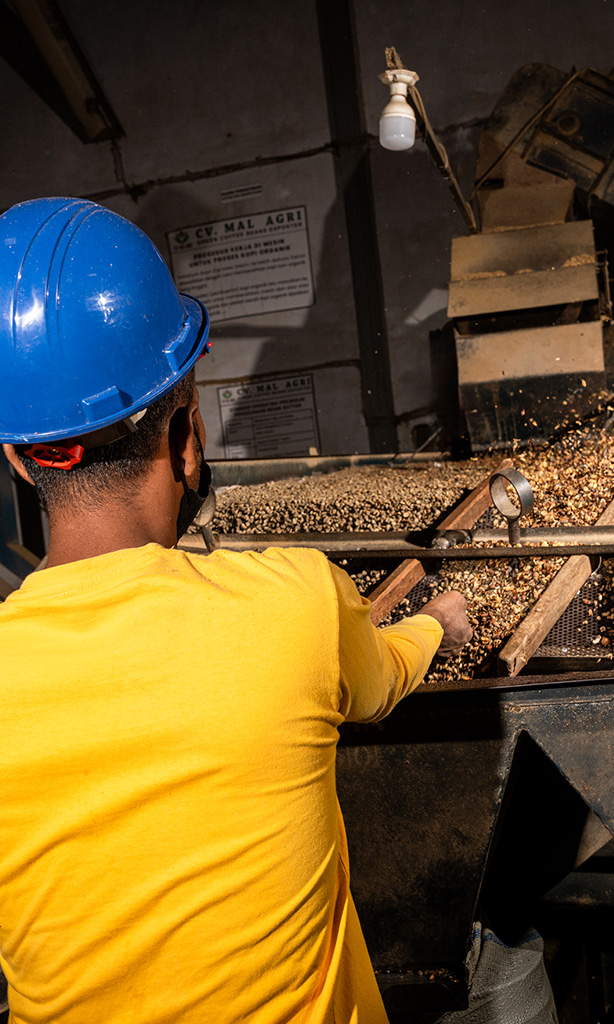
After reaching the appropriate moisture content, the coffee undergoes a grading process to ensure more uniform and consistent quality. With a grading capacity of 1.5–2 tons per hour, the beans are sorted based on size, density, and physical quality. This process helps ensure each batch meets consistent quality standards and is ready for international market demand.
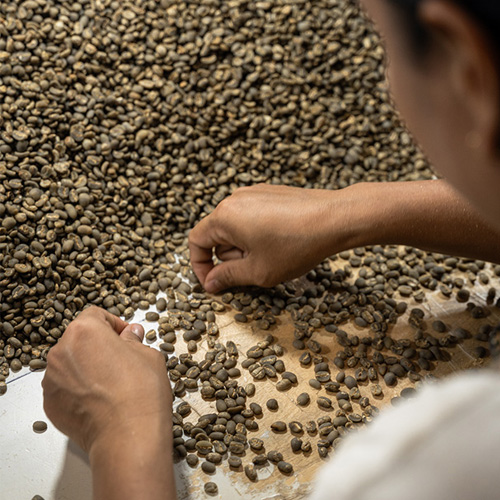
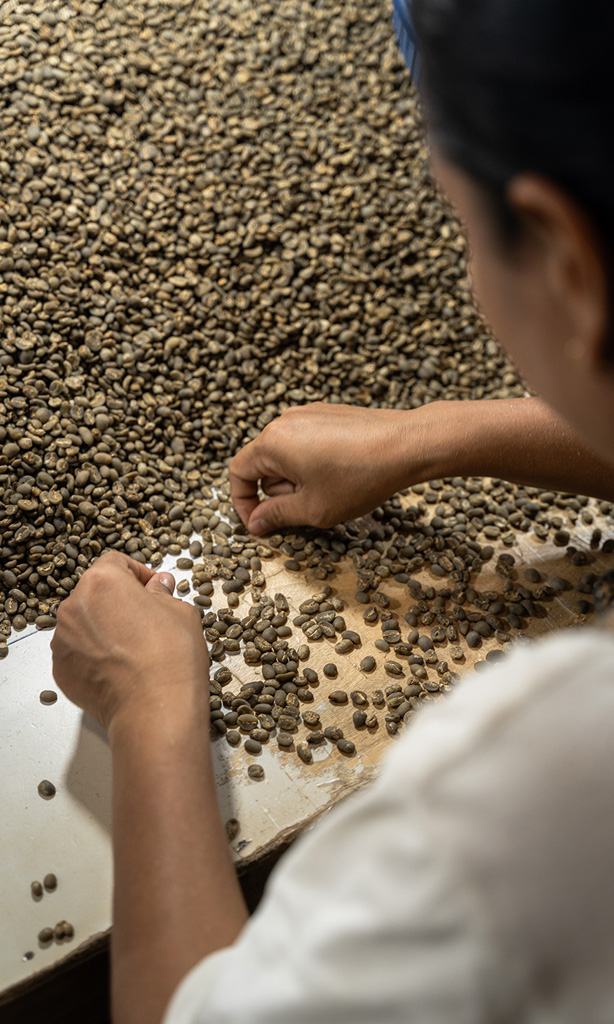
While technology improves efficiency, we believe the highest quality still requires a human touch. Each lot undergoes manual sorting by a trained team, with a capacity of up to 6 tons per day. Every bean is visually inspected to reduce defects and ensure only coffee that meets our quality standards proceeds to the next stage.
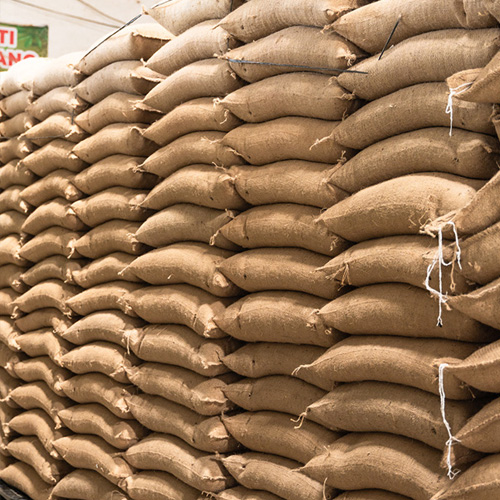
Once the coffee meets our quality standards, it is carefully packed in durable, moisture-resistant bags. Each lot is properly labeled and prepared to maintain quality during storage and transportation.
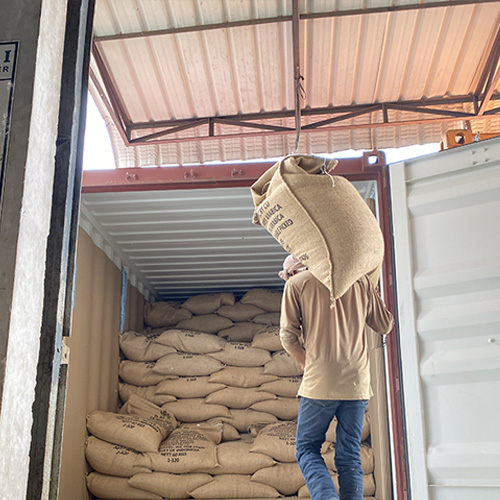
Once ready for shipment, the coffee is carefully loaded into containers under controlled conditions. Each lot is arranged securely to protect the coffee and maintain its quality throughout transportation to international destinations.
Member of :
+62 812 6217 9667